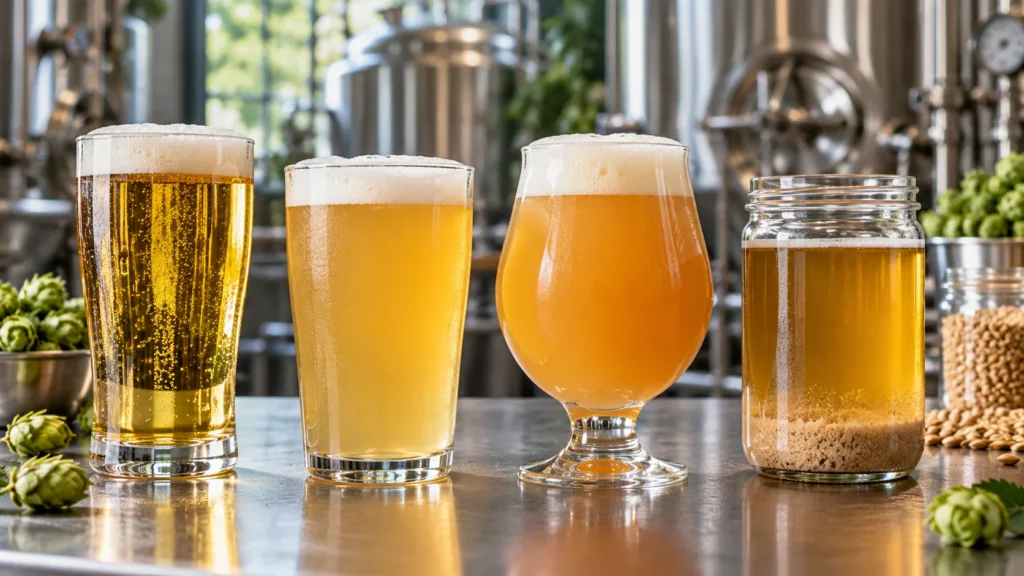
Beer clarity is not simply a cosmetic detail.
The appearance of a finished beer can reveal a great deal about the brewing process, including wort production, protein management, yeast performance, dry hopping, clarification, packaging and storage stability.
A bright, brilliantly clear lager is expected to look very different from a traditional Hefeweizen or a modern Hazy IPA. For this reason, haze is not automatically a defect.
The important question is:
Is the level and type of haze appropriate for the intended beer style?
Unwanted turbidity can originate from many different sources:
- suspended yeast;
- protein–polyphenol complexes;
- chill haze;
- starch;
- hop particles;
- dry-hop polyphenols;
- microbial contamination;
- poor trub separation;
- unstable colloidal material;
- sediment disturbed during packaging or serving.
Correcting a clarity problem therefore starts with identifying what is actually causing the haze.
This guide explains the major forms of beer haze and sediment, how to diagnose them, and how to improve clarity without unnecessarily stripping flavor, aroma or body from the beer.
1. Beer Clarity Is a Style-Dependent Quality
A clear beer is not always a better beer.
Brilliant clarity is normally desirable in styles such as:
- German Pils;
- Czech Pale Lager;
- Kölsch;
- Helles;
- Vienna Lager;
- many British bitters;
- American Pale Ale.
Visible haze may be completely appropriate in:
- Weissbier;
- Witbier;
- Hazy IPA;
- NEIPA;
- some heavily dry-hopped beers;
- certain farmhouse styles.
A beer should therefore be evaluated against its intended style rather than against a universal standard of brilliance.
A crystal-clear Hefeweizen may actually look less traditional than a naturally hazy one.
Likewise, a permanently cloudy German Pils can indicate a process or stability problem.
2. Quick Diagnostic Guide to Beer Haze and Sediment
3. What Actually Makes Beer Hazy?
Beer is a chemically complex colloidal system.
Even when beer appears clear to the eye, it contains many dissolved and extremely small dispersed substances.
Potential haze-forming material includes:
- proteins;
- peptides;
- polyphenols;
- yeast cells;
- hop particles;
- starch;
- beta-glucans;
- lipids;
- minerals;
- microorganisms.
Some of these substances remain stable in solution.
Others interact with one another and form increasingly large particles.
Once the particles become large enough to scatter visible light, the beer appears cloudy.
This is why beer haze is often less about a single ingredient and more about interactions between several components.
4. Chill Haze
Chill haze is one of the most common clarity problems in otherwise well-made beer.
Its defining characteristic is simple:
the beer becomes hazy when cold but clears again when warmed.
What causes chill haze?
Chill haze is mainly associated with interactions between haze-active proteins and polyphenols.
At lower temperatures, these compounds can form weak reversible associations.
The resulting particles scatter light and make the beer appear cloudy.
When the beer warms, those weak associations may separate again and the beer becomes clear.
Why chill haze matters
Chill haze is not usually dangerous and may have little immediate effect on flavor.
However, it can indicate limited colloidal stability.
Over time, repeated interactions between proteins and polyphenols may become stronger and less reversible.
A beer that initially develops only temporary chill haze can eventually develop permanent haze.
Chill Haze vs Permanent Haze
5. Protein Haze
Proteins are essential to beer.
They contribute to:
- foam formation;
- foam stability;
- body;
- mouthfeel;
- yeast nutrition;
- colloidal structure.
The goal is therefore not to remove all protein.
Problems occur when an excessive amount of haze-active protein remains available to interact with polyphenols.
Sources of haze-active protein
The quantity depends on:
- malt variety;
- malt modification;
- wheat content;
- oat content;
- rye content;
- mash schedule;
- wort separation;
- boil performance;
- hot break formation;
- cold break removal.
Wheat-rich and oat-rich beers naturally contain more material capable of contributing to haze.
This is one reason it would be inappropriate to apply the same clarity expectations to a Hefeweizen and a German Pils.
6. Polyphenols and Beer Haze
Polyphenols come mainly from:
- malt husks;
- hops.
They play multiple roles in beer.
At appropriate levels they may contribute to:
- flavor structure;
- mouthfeel;
- antioxidant activity;
- bitterness perception.
At higher levels they can also contribute to:
- astringency;
- haze;
- sediment formation;
- colloidal instability.
Polyphenols can bind with proteins, producing complexes that grow into haze-forming particles.
This process is particularly important in heavily hopped beer.
7. Dry Hopping and Hop Haze
Modern dry-hopped beer presents a special case.
Large dry-hop additions introduce:
- hop particles;
- polyphenols;
- proteins;
- enzymes;
- resins;
- other colloidal material.
A heavily dry-hopped beer may therefore remain hazy even when yeast sedimentation is otherwise complete.
This is not automatically a brewing error.
In NEIPA and Hazy IPA, a stable haze can be part of the intended style.
However, if the goal is a clear American Pale Ale or West Coast IPA, excessive hop-derived haze may be undesirable.
Factors increasing dry-hop haze
- very large dry-hop rates;
- fine hop particulate carryover;
- short settling time;
- transferring beer immediately after dry hopping;
- highly protein-rich grain bills;
- strong protein–polyphenol interaction;
- repeated agitation of hop material.
Practical control
After dry hopping:
- allow sufficient settling time;
- avoid unnecessary agitation;
- cold condition if style allows;
- transfer above the sediment layer;
- reduce physical hop material carryover.
8. Yeast Haze
Suspended yeast is one of the simplest and most common causes of cloudy beer.
Different yeast strains have very different flocculation characteristics.
High-flocculation yeast
These strains tend to:
- aggregate efficiently;
- settle relatively quickly;
- form a compact sediment.
Low-flocculation yeast
These strains remain suspended longer and may produce persistent turbidity.
This is not necessarily a defect.
Many wheat beer strains are intentionally poor flocculators.
Factors affecting yeast sedimentation
- yeast strain;
- calcium level;
- fermentation health;
- final gravity;
- temperature;
- beer pH;
- alcohol content;
- time;
- vessel movement.
Cooling generally promotes sedimentation of many brewing yeast strains.
Yeast Suspension Troubleshooting
9. Starch Haze
Starch haze is different from protein haze and yeast haze.
It can occur when starch survives the mash without being fully converted into soluble sugars and dextrins.
Possible reasons include:
- incomplete conversion;
- inadequate mash time;
- poor crush or mixing;
- insufficient enzymatic power;
- unsuitable mash temperature;
- starch entering the wort from adjuncts;
- excessive grain material passing into the kettle.
Starch haze may appear as a persistent milky or cloudy character.
It will not normally disappear simply by warming the beer.
Preventing starch haze
Focus on:
- correct mash temperature;
- adequate mash duration;
- appropriate enzymatic malt content;
- good mixing;
- suitable adjunct handling;
- avoiding excessive flour and grain solids in the kettle.
If conversion is uncertain, an iodine test can be used during mashing as a basic qualitative check for residual starch.
10. Hot Break and Cold Break
Wort clarification begins before fermentation.
Hot break
During heating and boiling, proteins and other compounds aggregate into visible flocs.
A good hot break helps remove unstable material from wort.
Hot break formation depends on factors including:
- wort composition;
- boil intensity;
- pH;
- calcium;
- time.
Cold break
When hot wort is rapidly chilled, additional proteins, polyphenols and other compounds precipitate.
This is known as cold break.
Some cold break material in the fermenter is normally harmless.
However, carrying very large quantities of trub into fermentation can contribute to:
- excessive sediment;
- clarity problems;
- difficult transfers.
The objective is not necessarily to produce perfectly particle-free wort.
The goal is reasonable trub management.
11. Kettle Finings
Kettle finings are used during the boil to promote aggregation of proteins and other haze-forming material.
Common products include:
- Irish moss;
- carrageenan-based products;
- tablet forms such as Whirlfloc-type finings.
They are usually added near the end of the boil.
The exact dose and timing should follow the manufacturer’s instructions because formulations differ.
What kettle finings do
They help small particles combine into larger flocs.
Larger flocs:
- settle more easily;
- separate more efficiently;
- improve wort clarity;
- may improve final beer clarity.
Kettle finings are not a substitute for:
- proper mashing;
- healthy fermentation;
- good cold conditioning;
- correct packaging.
12. Cold Crashing
Cold crashing means rapidly reducing the temperature of fermented beer before packaging.
The main goals are to encourage:
- yeast sedimentation;
- protein precipitation;
- hop particle settling;
- compact trub formation.
For many ales, brewers commonly cool the beer to approximately 0–4°C when their equipment allows it.
A typical cold-conditioning period can range from roughly 1 to several days, depending on:
- yeast strain;
- beer composition;
- fermenter geometry;
- desired clarity.
There is no universal requirement for an exact number of hours.
Important oxygen warning
Cooling beer causes the gas inside the fermenter to contract.
If the vessel is not pressure-capable or protected by CO₂, outside air may be drawn into the fermenter.
This is especially undesirable for:
- IPA;
- NEIPA;
- Pale Ale;
- other oxidation-sensitive beers.
Cold crashing can therefore improve visual clarity while simultaneously creating an oxidation problem if gas management is poor.
Cold Crash: Benefits and Risks
13. Gelatin Finings
Gelatin is a common clarification aid in homebrewing.
It is positively charged under normal beer conditions and can interact with negatively charged haze-forming particles.
Gelatin is particularly effective for helping:
- yeast;
- proteins;
- other suspended material
settle more rapidly.
General procedure
The exact method varies, but typically:
- gelatin is hydrated in clean water;
- it is gently heated to dissolve;
- it is added to cold or cooling beer;
- the beer is allowed to settle before transfer.
Avoid boiling gelatin unnecessarily.
The required dose varies by product, beer composition and desired clarity, so a fixed universal gram-per-liter recommendation is not appropriate.
Potential disadvantage
Gelatin is animal-derived.
This matters if the beer is intended to be:
- vegetarian;
- vegan.
14. Isinglass
Isinglass is another traditional fining agent.
It is derived from collagen and is particularly effective for flocculating yeast.
Historically, it has been widely associated with British cask beer.
Its main purpose is to improve rapid yeast sedimentation and beer brightness.
As with gelatin, it is animal-derived and therefore not suitable for vegan beer.
15. Silica-Based Finings
Silica-based clarification products primarily target haze-active proteins.
They can be useful when protein haze is an important concern.
Compared with yeast-targeted finings, they act on a different part of the haze system.
This illustrates an important principle:
different finings solve different clarity problems.
A fining agent that works extremely well for suspended yeast may not be the best solution for protein–polyphenol instability.
16. PVPP
PVPP — polyvinylpolypyrrolidone — is used to bind polyphenols.
It can therefore improve colloidal stability where polyphenol-driven haze is a concern.
PVPP is more common in commercial stabilization but the principle is important for advanced homebrewers as well.
Protein-targeted and polyphenol-targeted treatments are sometimes used together because haze often forms through interactions between the two.
17. Biofine and Similar Clarifiers
Silicic-acid-based products sold as Biofine-type clarifiers are popular because they can accelerate clarification without animal-derived ingredients.
They can promote sedimentation of haze-forming material and are often used in cold beer before packaging.
As with all finings:
- dose matters;
- beer temperature matters;
- contact time matters;
- product formulation matters.
Follow the manufacturer-specific instructions rather than assuming that all liquid finings have identical strength.
18. Comparing Beer Clarification Methods
19. Sediment in Bottled Beer
Sediment in bottle-conditioned beer is normal.
During bottle conditioning, yeast ferments priming sugar and produces:
- CO₂;
- a small amount of additional ethanol;
- new yeast biomass.
Some yeast then settles to the bottom of the bottle.
This sediment is not automatically a defect.
Excessive sediment can result from
- transferring too much yeast;
- transferring trub;
- hop particles in the bottling beer;
- bottling immediately after dry hopping;
- inadequate settling time;
- excessive priming yeast.
Reducing bottle sediment
Before bottling:
- allow fermentation to finish completely;
- give yeast time to settle;
- cold condition if appropriate;
- avoid disturbing the sediment layer;
- transfer gently from above the trub.
Some bottle-conditioned beer will still develop a visible yeast layer.
That is normal.
20. Sediment in Kegs
Kegs can also collect:
- yeast;
- protein material;
- hop particles;
- cold-break-like precipitates.
The first pour may therefore be cloudier than later pours.
This depends heavily on:
- keg geometry;
- dip tube position;
- whether the keg was moved;
- amount of sediment transferred.
Reducing keg sediment
- cold crash before transfer;
- transfer above the fermenter sediment;
- avoid transferring hop sludge;
- allow the keg to settle cold;
- avoid moving it unnecessarily before serving.
Floating dip tubes can also help draw clearer beer from the upper portion of the keg.
21. Hop Particles in Finished Beer
Visible hop particles are a physical sediment problem rather than a true molecular haze.
They can enter packaged beer when:
- dry-hop pellets break apart;
- the beer is transferred too soon;
- hop bags or spiders release fine material;
- sediment is disturbed during transfer.
Hop particles can contribute to:
- rough mouthfeel;
- vegetal character;
- excessive polyphenols;
- gushing in extreme cases;
- blocked poppets or dip tubes.
Allowing the beer to settle and using controlled transfers is usually more effective than trying to filter out every particle mechanically.
22. Microbial Haze
Microbial haze deserves special attention because it may indicate instability rather than a purely cosmetic problem.
Possible organisms include:
- wild yeast;
- Lactobacillus;
- Pediococcus;
- Acetobacter;
- other contaminating organisms.
Microbial haze may be accompanied by:
- unexpected sourness;
- phenolic character;
- changing gravity;
- continued carbonation;
- overpressurization;
- pellicle formation;
- unusual aroma development.
If a packaged beer becomes progressively cloudier while its flavor and carbonation are also changing, microbial contamination should be considered.
23. A Simple Temperature Test for Haze Diagnosis
One of the easiest homebrew tests is to compare the same beer at two temperatures.
Procedure
- Pour or collect two comparable samples.
- Keep one sample cold.
- Allow the second sample to warm toward room temperature.
- Compare visual clarity.
Interpretation
This test does not identify every haze source, but it provides useful diagnostic information.
24. Can Beer Be Too Clear?
Yes.
Aggressive clarification can sometimes remove compounds that contribute positively to:
- body;
- foam;
- aroma;
- flavor stability.
This matters especially in styles where haze is part of the intended structure.
Trying to make a NEIPA brilliantly clear can be counterproductive.
The goal should never be:
maximum clarity at any cost.
The correct goal is:
appropriate visual stability for the intended beer.
25. Clarity and Foam Stability
Protein management should be balanced carefully.
Some proteins contribute to haze, but some also contribute to foam stability.
Overly aggressive protein removal may therefore have consequences for head retention.
This is another reason why clarification should be targeted rather than indiscriminate.
A brewer should identify the haze source first and then choose the least disruptive solution.
26. Clarity and Brewing Water
Water chemistry can indirectly influence clarity.
Important factors include:
- calcium;
- pH;
- alkalinity.
Calcium can support several brewing reactions, including:
- protein precipitation;
- yeast flocculation;
- mash chemistry.
Mash pH and wort pH also influence protein behavior and hot-break formation.
Water chemistry alone will not solve every clarity problem, but poor water management can make clarification more difficult.
27. Clarity and Mash pH
Mash pH affects:
- enzyme performance;
- protein behavior;
- wort composition;
- extraction.
A mash operating significantly outside the appropriate pH range can contribute to:
- inefficient conversion;
- excessive extraction;
- weak hot break;
- unstable wort composition.
Clarity should therefore be considered part of the complete brewing process rather than as a correction performed only after fermentation.
28. Practical Clarification Workflow
For a beer intended to be clear, a reliable process is more important than applying large amounts of finings.
29. Common Mistakes When Trying to Clear Beer
1. Treating every haze as yeast
Protein haze, starch haze and microbial haze will not necessarily respond to a yeast-targeted fining.
2. Using finings before diagnosing the problem
A clarification product should solve a specific problem.
3. Cold crashing before fermentation is complete
This can interrupt yeast cleanup and create other fermentation defects.
4. Introducing oxygen during cold crash
Visual clarity is not worth sacrificing flavor stability.
5. Transferring directly from disturbed sediment
Even brilliantly clear beer can become cloudy again within seconds.
6. Expecting heavily dry-hopped beer to behave like lager
Large quantities of hops change the colloidal structure of beer.
7. Filtering too aggressively
Excessive filtration or fining can remove desirable flavor and body.
30. When Should You Actually Worry About Sediment?
Sediment alone is not necessarily a problem.
Normal sediment can include:
- yeast;
- proteins;
- hop fragments;
- trub;
- bottle-conditioning yeast.
Sediment becomes more concerning when it is associated with:
- continuing fermentation after packaging;
- excessive pressure;
- unusual odors;
- unexpected acidity;
- ropey texture;
- rapidly changing flavor;
- recurring contamination.
The visual appearance should therefore always be considered together with:
- aroma;
- flavor;
- gravity;
- carbonation;
- package stability.
31. Final Troubleshooting Matrix
32. Conclusion: Clear Beer Starts Long Before Packaging
Beer clarity is the result of the entire brewing process.
A brewer cannot reliably produce bright, stable beer simply by adding a fining agent at the last moment.
Good clarity begins with:
- complete mash conversion;
- appropriate mash and wort pH;
- effective boiling;
- good hot-break formation;
- efficient cooling;
- controlled fermentation;
- suitable yeast selection;
- sufficient conditioning;
- careful dry hopping;
- effective sediment management;
- low-oxygen transfer.
The most important diagnostic distinction is between intentional haze and unwanted haze.
A cloudy Hazy IPA may be exactly what the brewer intended.
A cloudy Pilsner may require investigation.
Chill haze points toward protein–polyphenol instability.
Yeast haze points toward flocculation and conditioning.
Hop haze may be linked to heavy dry hopping.
Starch haze suggests conversion problems.
Microbial haze may indicate a much more serious stability issue.
Once the type of haze is identified, clarification becomes much easier to manage.
The goal is not to make every beer brilliantly clear.
The goal is to produce:
the appropriate appearance, stability and sediment level for the beer you intended to brew.